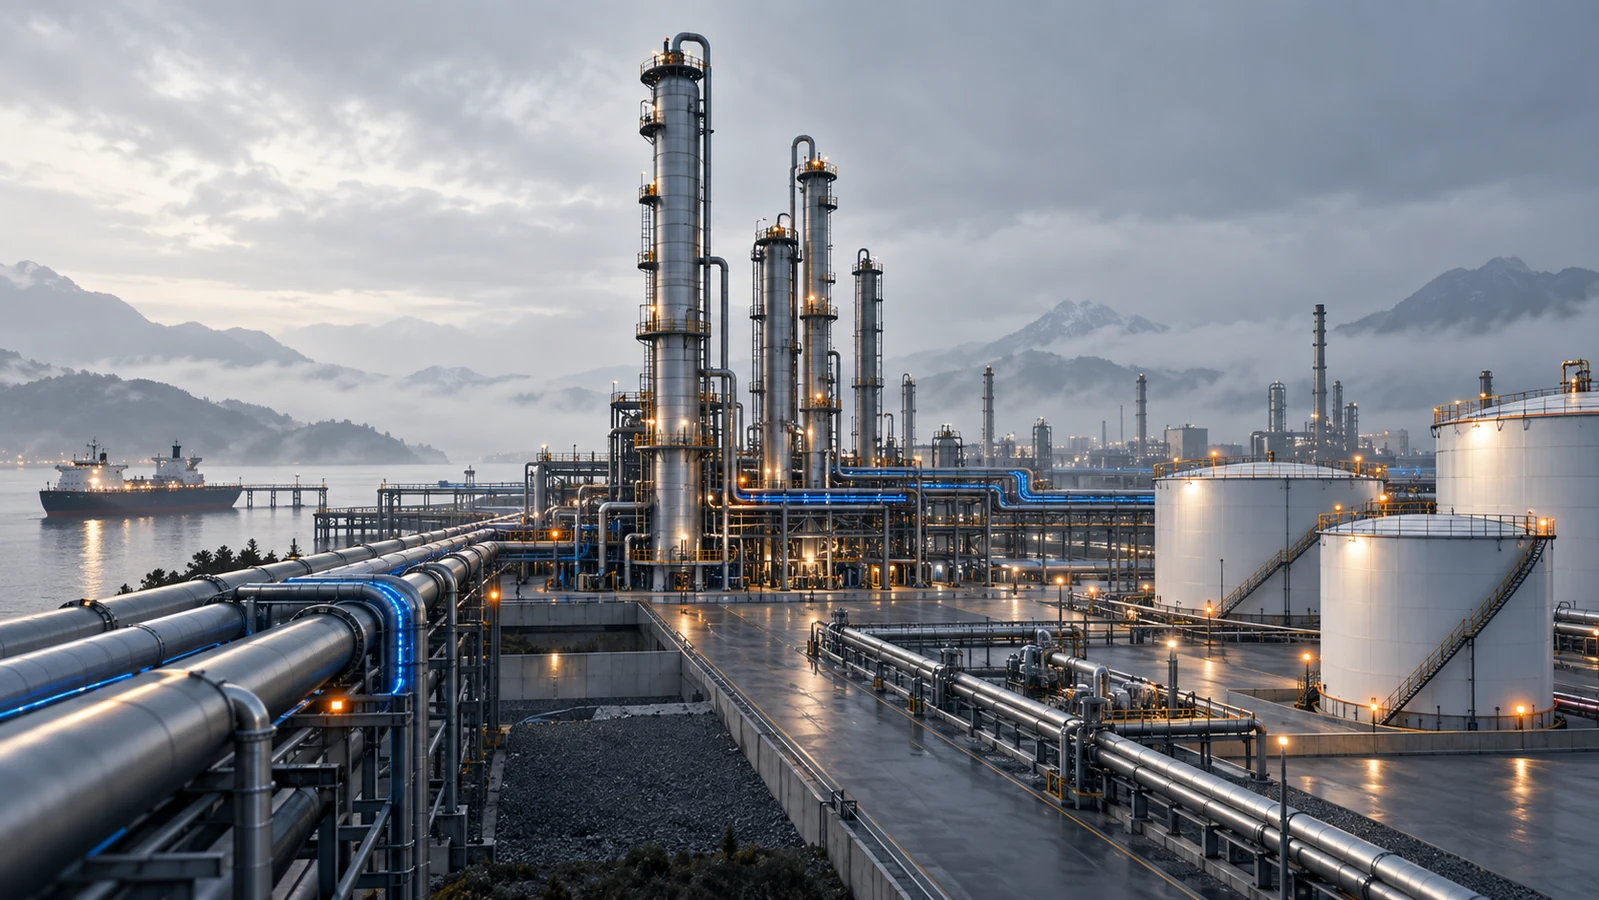
The Saveh complex processes gas condensate and petroleum products through distillation, sweetening and blending. Laboratory testing supports the conformity of incoming feedstock and finished products with technical specifications.
Testing the incoming feedstock
The laboratory monitors incoming raw materials and finished petroleum and lubricant products. Tests listed in the catalogue include distillation range, flash point, sulfur and mercaptan content.
Separation by boiling point
Continuous and batch distillation separate petroleum cuts by differences in boiling point. The unit processes gas condensate, solvents, kerosene and other petroleum products.
The equipment includes one continuous tower and two batch towers. Nominal daily capacities are 500 tonnes for continuous distillation and 120 tonnes for batch distillation.
Reducing undesirable sulfur compounds
The sweetening unit uses oxidative desulfurization (ODS) to remove or reduce undesirable sulfur compounds. The catalogue also describes wastewater management and odor-emission control measures.
Blending to technical specifications
The blending unit combines petroleum and chemical feedstocks, intermediate streams and processed cuts to achieve the required product properties. Formulation, real-time quality control and flexibility for varying feedstocks are central to the process.